-


-


-
-


whatsapp
-
WeChat
A batch of HEPA filters with gel seal for the modernization and reconstruction of clean rooms of a large pharmaceutical enterprise.
2026-07-01
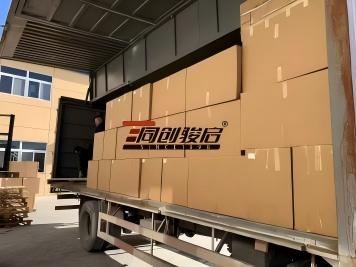
Our company has a batch of medical products with high leak-tightnessHEPA filter with gel sealUpon completion of the full production cycle, purity testing and packaging as per standards, the products were systematically loaded into vehicles using forklifts and sent directly to the clean production facilities of leading domestic pharmaceutical companies. This batch of gel seal HEPA filters has been specifically designed for GMP compliant pharmaceutical cleanrooms; Featuring a silicone gel seal design that provides complete sealed filtration, these products meet stringent cleanliness requirements for processes such as active pharmaceutical ingredient (API) synthesis, drug compounding and dispensing, and aseptic filling, thereby ensuring the required level of filtration to maintain sterile air on the manufacturing floor.

This off-the-shelf, high-performance filter is designed specifically for the pharmaceutical industry and features a gel seal channel with a blue gasket. It uses low-dust fiberglass filter media; The filter is compatible with air purification systems in sterile production facilities that comply with GMP standards.
I. General information about the project: strict requirements for the tightness of filtration systems in pharmaceutical workshops (GMP standard)
The pharmaceutical company participating in this project operates several production lines for the production of sterile drugs and active pharmaceutical ingredients (API). In the facility's existing cleanrooms, high-efficiency filters suffered from persistent problems such as air leaks around the perimeter of the frame and seal failures. As a result, the concentration of dust particles and microorganisms often approached the critical limits established by GMP standards, creating the risk of product contamination and defective batches.
The engineering service of the enterprise, responsible for the operation of clean rooms, formulated three mandatory requirements for purchased equipment:
1. The design of the filters must ensure complete tightness, eliminating the possibility of unfiltered air entering the clean area bypassing the filter element;
2. The filter material must have low volatility and minimal dust separation, and not emit harmful substances, which is necessary to comply with the standards for the production of sterile pharmaceuticals;
3. Filtration efficiency must consistently meet the requirements for Class 100 and Class 10,000 cleanrooms.
After conducting a series of tests for tightness and a comparative assessment of air purity by independent experts, the customer decided to cooperate with our companyHEPA filter with gel seal
These units were purchased in bulk as primary filtration equipment to upgrade the ventilation systems in the filling room, sterile buffer room and testing laboratory.
II. Key Benefits of Gel Seal HEPA Filters: Solution for Sterile Pharmaceutical Processing
These gel seal HEPA filters are specifically optimized to meet pharmaceutical GMP standards and offer a number of design and performance advantages:
1. Gel seal design (silicone): eliminate the risk of air leakage
The filter has a built-in gel seal channel; Liquid silicone is poured directly during installation on site, forming a seamless sealed layer. Unlike standard rubber gaskets, this design completely eliminates leakage at the edges of the frame, effectively preventing untreated air from entering the clean room. This provides reliable control of microorganisms and particles, meeting the strict GMP acceptance criteria set for pharmaceutical plants.
2. Ultra-fine glass fiber filter material: high filtration precision and no particle separation
The filter uses ultra-thin, high-density glass fiber material to consistently achieve the required 0.3 micron particle filtration performance and effectively capture bacteria, spores and dust aerosols. Before shipment, the material undergoes a purging procedure with clean air; During operation, it does not emit fibers or volatile organic compounds (VOCs), which prevents secondary contamination of pharmaceutical products or raw materials.
3. Lightweight aluminum alloy frame: easy to replace frequently in clean rooms
The filter has a lightweight bent aluminum alloy frame that is resistant to corrosion and deformation. Thanks to the built-in positioning clamps, installation and replacement can be carried out by one person. This significantly reduces cleanroom downtime during upgrades and minimizes economic losses associated with interruptions in pharmaceutical production. Standardized dimensions allow direct replacement of outdated HEPA filters without the need to remodel ceiling ventilation units.
4. Stable performance over a wide temperature range: suitable for environments with constant temperature and humidity
The filter material and sealing system are designed for stable and long-term operation in clean rooms with a temperature of 18–26°C and a humidity of 45–65%. The sealing material does not harden, does not shrink or crack, maintaining tightness throughout its entire service life; this extends filter life and reduces pharmaceutical manufacturers' costs for maintenance and consumables.

The gel seal HEPA filters were packaged in boxes on pallets and carefully loaded using a forklift for direct shipment to the pharmaceutical cleanroom refurbishment site.
III. Dedicated quality control in clean room conditions and protective packaging to ensure proper quality when supplied to pharmaceutical companies.
In accordance with the high standards of purity required for pharmaceutical products, this batch was manufactured in accordance with the following requirementsHEPA filter with gel sealCompliance with specialized production and testing protocols for cleanroom equipment:
1. All products are assembled in a Class 10,000 clean room to prevent dust contamination during the manufacturing process. Before shipment, each filter undergoes a PAO (polyalphaolefin) leak test to ensure no leaks; Based on the test results, a detailed report is drawn up, which is necessary for pharmaceutical companies for acceptance according to GMP standards and for maintaining documentation.
2. Finished products are packaged in two-layer antistatic polyethylene film with vacuum sealing to protect them from external dust. The outer packaging consists of boxes made of reinforced heavy-duty cardboard, mounted on solid wood pallets; Such packaging prevents damage to the filter material and deformation of the sealing channels due to impacts during transportation.
3. During loading, forklifts move at low speed to ensure smooth operations, and personnel check model specifications and quantities individually (pallet by pallet). The package includes installation instructions and leak test reports in Chinese and English, making it easy to accept, install and commission the equipment on site.
The use of completely enclosed vehicle transport minimizes the risk of dust and mechanical damage during intermediate overloads. Once products arrive on site, they can be immediately used for replacement or installation in cleanrooms, reducing production downtime required by a pharmaceutical company to upgrade facilities.
IV. Positioning in the pharmaceutical cleanroom market: increased focus on filtration solutions for GMP manufacturing areas
The pharmaceutical and biomanufacturing industries place the highest demands on the tightness and cleanliness of air filtration equipment. With extensive experience in the pharmaceutical, medical device and biological laboratory air purification industries, our company is ready to provide the solutions you needHEPA filter with gel seal,Pre-filter material (coarse/medium),Integrated filtration unit and complete cleaning kitAll products comply with GMP standards for use in clean rooms.
In the future, we will continue to improve the gel seal technology and optimize the compositions of low-outgassing filter materials. We remain committed to providing high-performance filters—with superior sealing and consistent performance—to leading pharmaceutical companies and biological laboratories across the country, helping them to consistently meet aseptic manufacturing standards and reduce the risks associated with pharmaceutical contamination.