-


-


-
-


whatsapp
-
WeChat
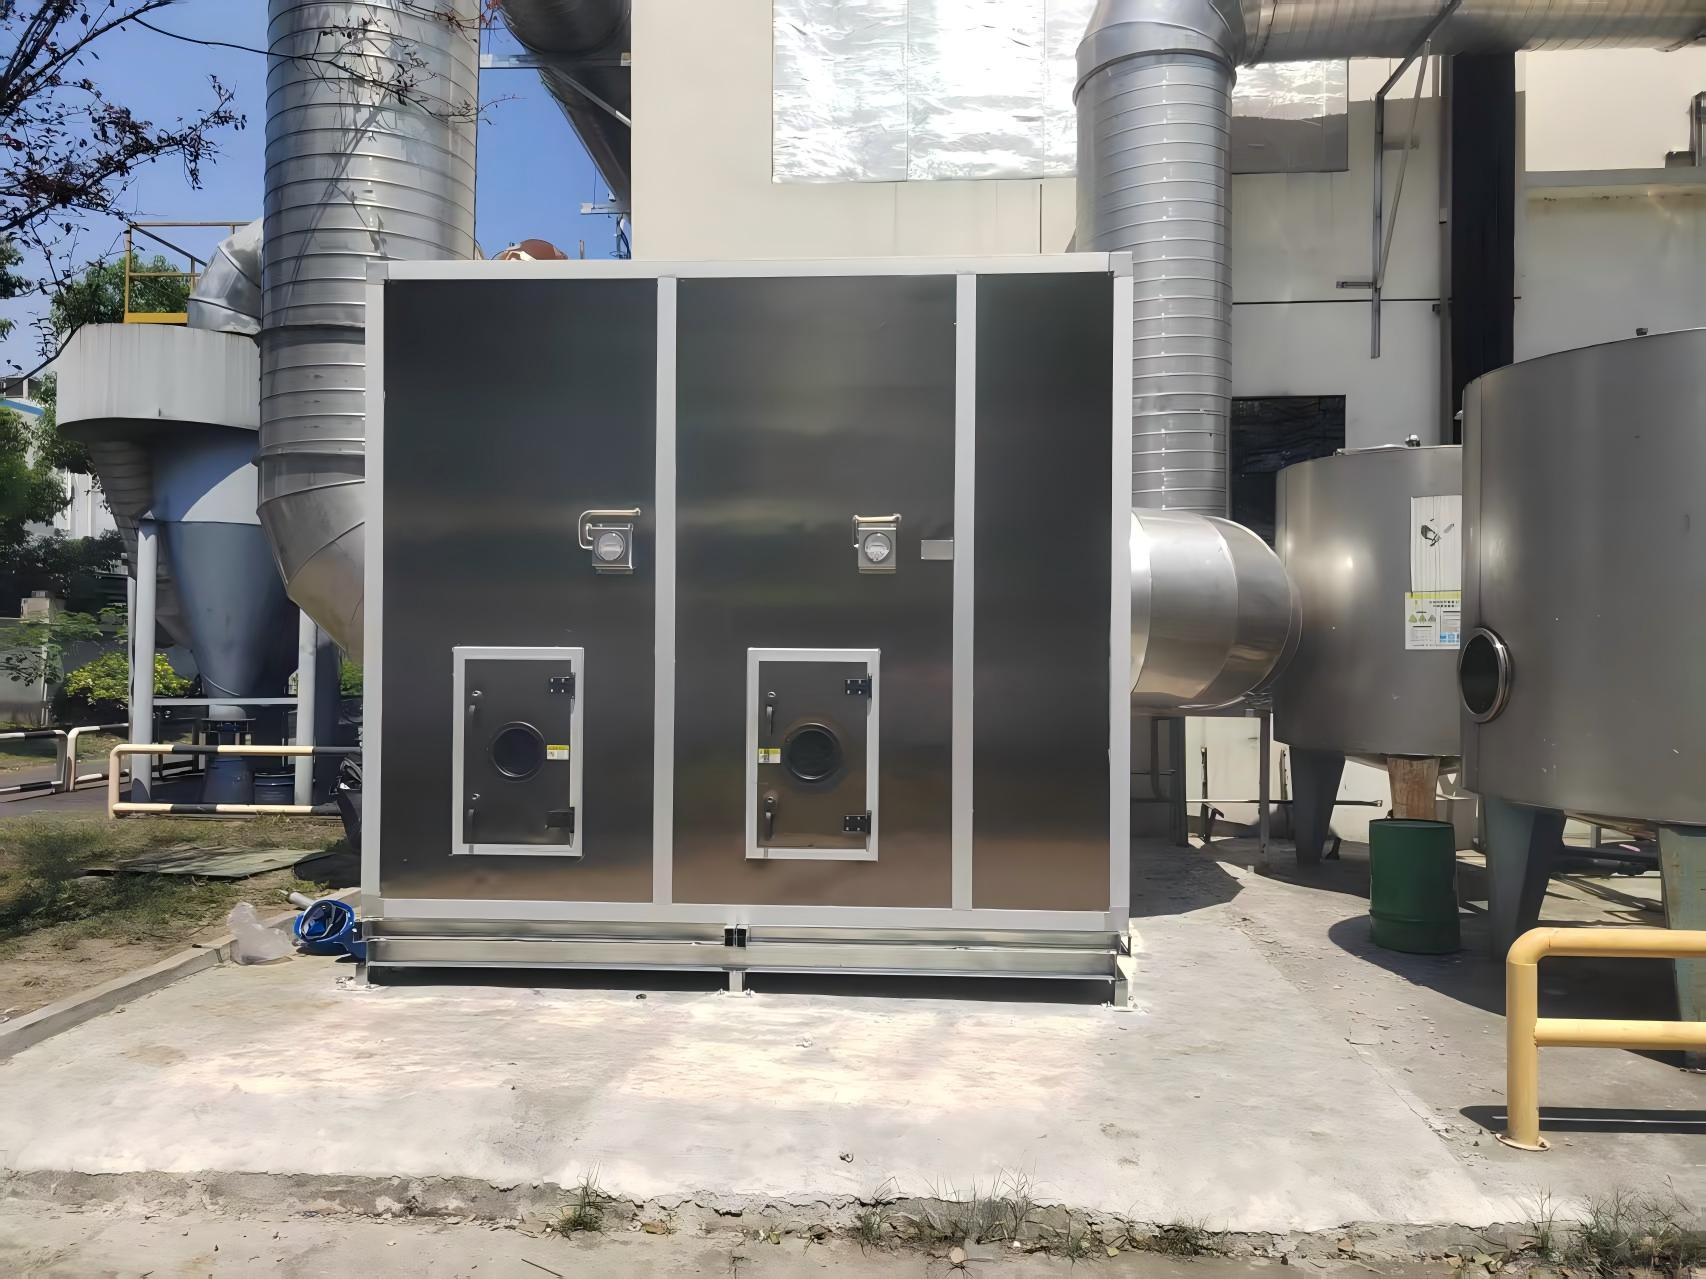
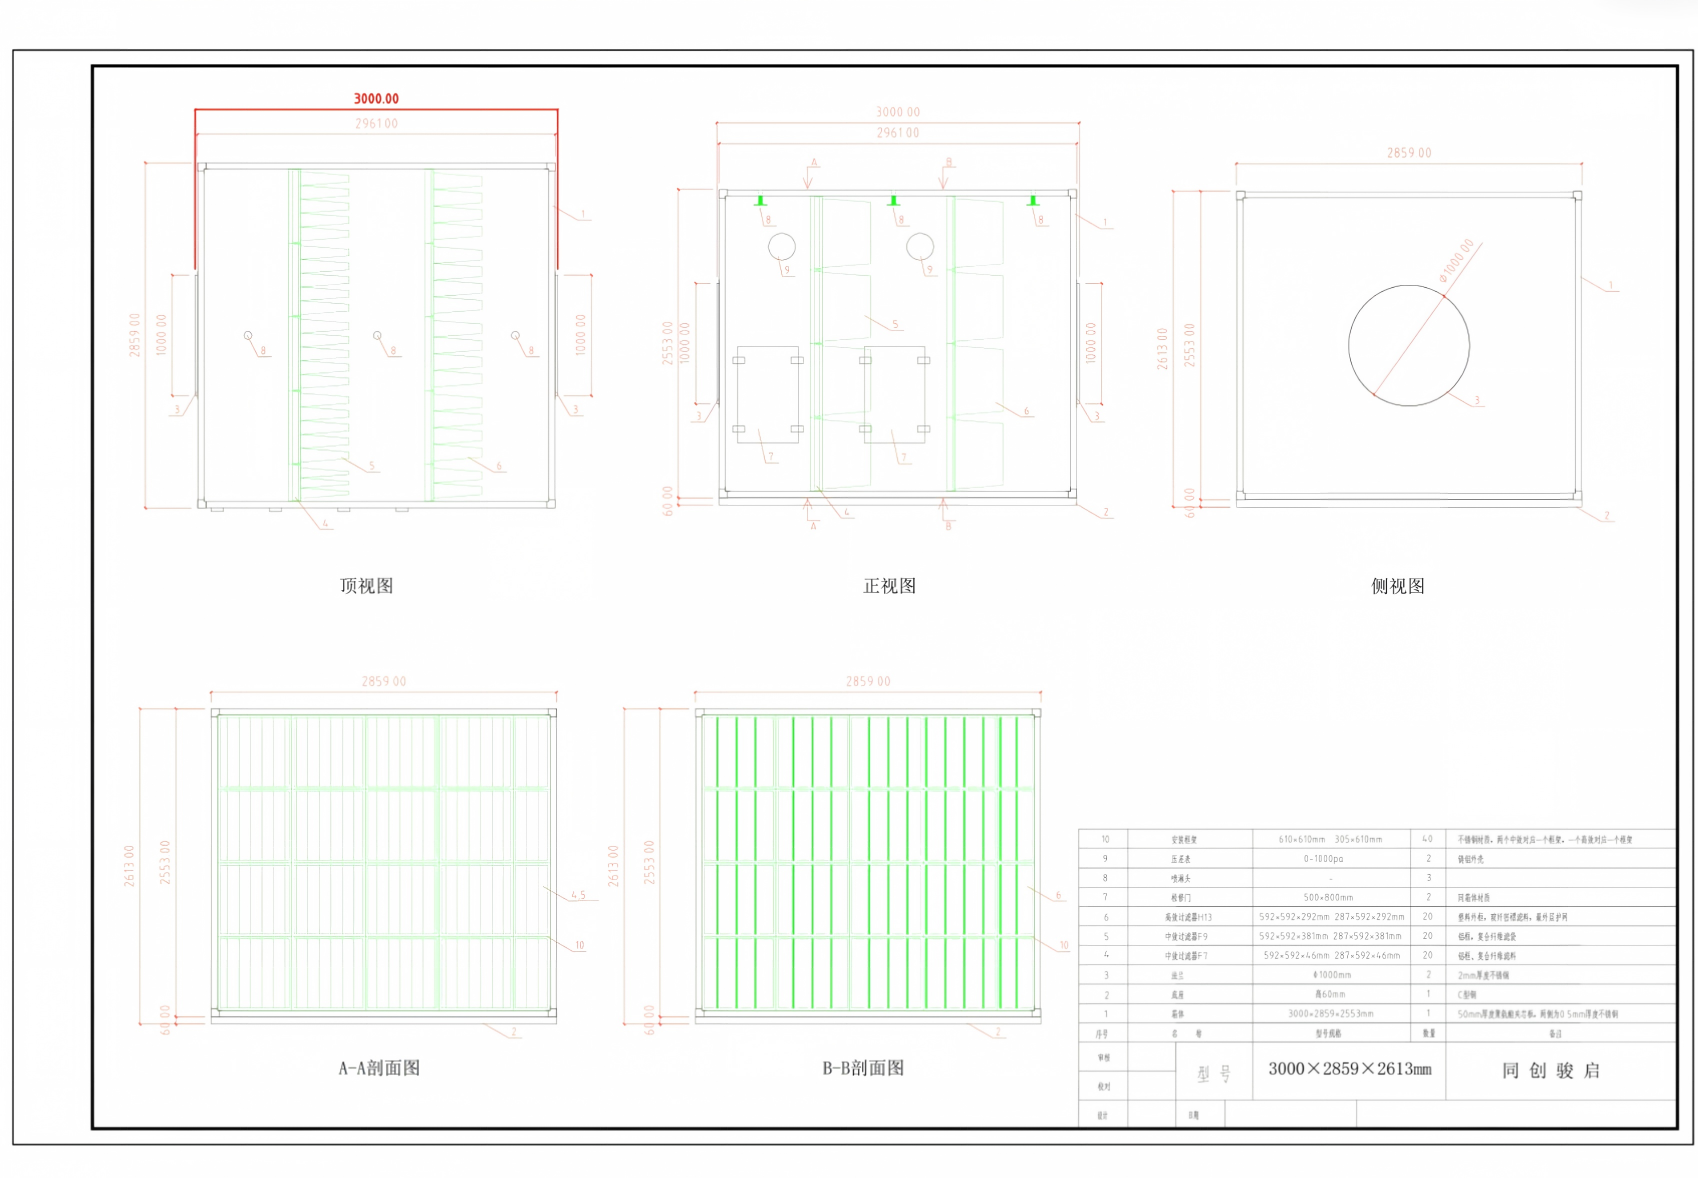
The direct-to-chip component project uses low-efficiency filters for the entire vehicle, creating an environmentally friendly line of defense for semiconductor manufacturing.
2026-06-17
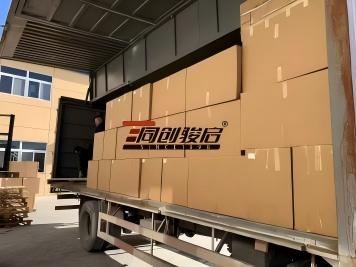
Recently, our company manufactured a batch of [goods/products] to an individual order from a leading domestic chip manufacturer Ultra High Efficiency FiltrationProduction, quality control and packaging of the equipment have been completed. The entire batch is packaged and ready to be sent directly to the customer’s site. The supplied products will serve as the primary filtration equipment in the chip shop cleanroom ventilation system, providing a consistent supply of high-purity air for high-precision processes such as silicon wafer manufacturing and photolithography. This is another important confirmation of our company's commitment to serving the high-tech semiconductor manufacturing sector.

The specially designed ultra-high efficiency filter was packaged and shipped directly to the chip project site.
I. Background of the project: Strict requirements for air purity in the production of microcircuits
Microchip production is one of the industries with the highest environmental requirements. Dust and particulate matter in the air, settling on the surface of the wafers, can cause short circuits and lithography defects, directly affecting the yield of usable microcircuits. The chip foundry we work with has set extremely high standards for the filtration level, stability and weather resistance of the ventilation system of their new production line: the filters must not only provide ultra-high efficiency, but also meet requirements such as low air resistance, long service life and low dust generation to ensure long-term stable operation of the production line.
After several rounds of random testing and operating conditions, the client ultimately chose our companyUltra high efficiency filterAs a primary filtration device, our technical team has specifically optimized the product for the unique operating conditions of chip shops. This ensures that the filtration efficiency and operational stability meet the needs of the production line with high air flow and high cleanliness requirements.
II. Key Product Benefits: Designed for semiconductor industry cleanroom scenarios
Introduced this time, the sub-HEPA filter is a specialized product optimized for high-tech cleanrooms. Its main advantages are reflected in the following aspects:
Highly efficient filtration:The use of fiberglass composite filter media consistently meets 0.3 micron particle filtration efficiency standards, effectively capturing dust and aerosol contaminants, providing a high-purity air environment for chip manufacturing processes and ensuring satisfactory product yield.
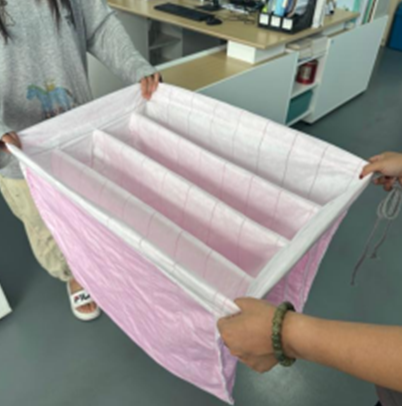
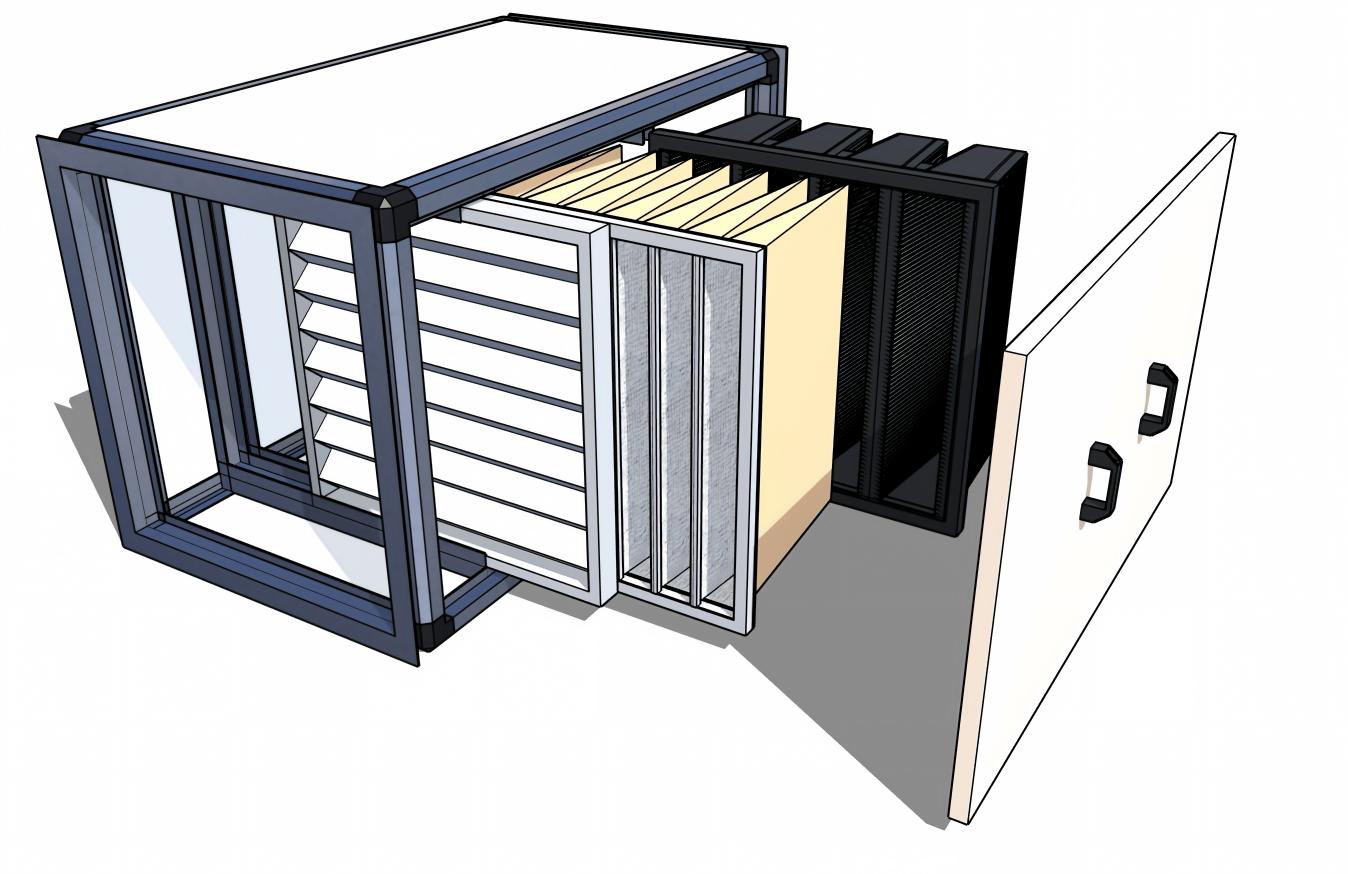
Low air resistance design:The use of V-shape/box design can maximize the deployment area of the filter media in a limited volume, effectively reducing the initial air resistance, reducing the power consumption of air conditioning fans and adapting to high air flow ventilation systems in chip manufacturing plants.
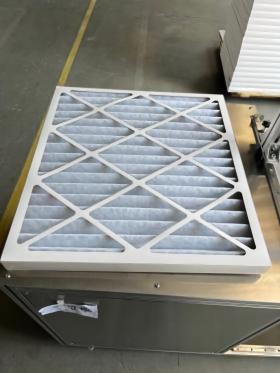
Highly adaptable mounting design:Adopts ABS/Aluminum alloy outer frame with special sealing strips to fit perfectly into the ceiling/cavity of the unit in the clean room after installation, eliminating the risk of air leakage and ensuring the overall efficiency of the filtration system.

The pre-engineered sub-HEPA filter, designed specifically for chip manufacturing plants, features a V-shape design, low air resistance and high dust holding capacity, making it suitable for large volume ventilation systems in cleanrooms.
III. Manufacturing and Delivery: Comprehensive Quality Control to Ensure High Quality Projects are Delivered
For this chip manufacturer order, our company has implemented exclusive quality control standards for high-tech projects:
Clean production and testing:The product manufacturing process is carried out in a class 10,000 clean room to avoid secondary contamination; Each filter is tested for air resistance, efficiency and airtightness before leaving the factory to ensure full compliance with the chip manufacturer's standards and strict acceptance criteria.
Individual packaging and protection:Finished products are packaged in double-layer antistatic polyethylene bags, reinforced with an outer cardboard box and pallet to prevent dust contamination and mechanical damage during transportation, ensuring that the product remains clean when delivered to the customer's site.
Efficient delivery by full truckloads:This order uses full truckload shipping with full enclosed protection to avoid the risk of contamination during loading and unloading; Transportation routes and times are planned in advance to ensure timely delivery of goods to the customer site without disrupting the production line installation schedule.
IV.Corporate sustainability and future prospectsAs a leading manufacturer specializing in industrial cleanroom filtration, our company has a long history of providing customized filtration solutions for high-tech industries such as semiconductor, pharmaceutical and precision manufacturing. The successful completion of this sub-HEPA filter project further demonstrates our capabilities in research and development, manufacturing and delivery of high quality cleanroom filtration products. Going forward, we will continue to deepen our expertise in high-tech manufacturing sectors such as the semiconductor industry and biopharmaceuticals, constantly optimizing the performance of our sub-HEPA and HEPA filters to provide more consistent quality and professional service, thereby supporting the implementation of more high-tech cleanroom projects and ensuring the high-quality development of China's manufacturing industry.